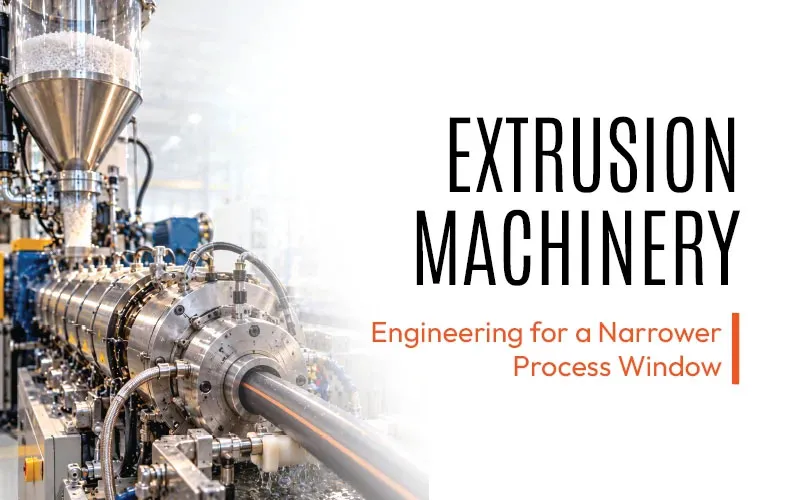
Cable extrusion is being asked to accommodate a wider production envelope. Manufacturers are processing more polymers, developing specialised cable constructions and serving applications with tighter dimensional and performance requirements. At the same time, pressure for higher output, material efficiency and lower operating costs remains high.
The result is a narrower and more demanding process window. HFFR and LSZH compounds can bring higher filler loading, different rheological behaviour and greater sensitivity to thermal conditions. XLPE and related materials introduce different requirements around dispersion, residence time, cooling and curing. Thermoplastic elastomers, PUR and engineering polymers add further processing requirements.
These requirements are influencing machinery design itself. Screw and barrel geometry, feeding, thermal management, tooling, cooling, curing and process control are increasingly being considered in relation to the material and application rather than as independent machine elements.
Dr. Mikko Lahti, R&D Director, Maillefer, describes the operating challenge in similar terms. “Today’s extrusion systems must cope with an unprecedented range of cable constructions, materials and application requirements.” He points to automotive electrification, renewable energy, HVDC transmission, data communication and fire-safe building cables as applications placing greater demands on materials, tolerances and production conditions. As cable designs become more material-efficient, acceptable process variation also becomes smaller. Maintaining output linearity, temperature control and dimensional consistency therefore becomes more consequential.
Material Behaviour Is Reshaping the Machine Material characteristics increasingly determine extrusion-system configuration.
HFFR and LSZH compounds are a clear example. Their formulations can contain high levels of mineral fillers, affecting melting, pressure management, thermal behaviour and wear. Davide Costabile, Area Manager, Wire & Cable Division, MFL Group, links this processing window to screw and extruder design, tooling, temperature control, cooling and overall line configuration. “…extrusion equipment can no longer be designed around a single ‘standard’ material,” he says.
Moisture control is another process variable that becomes more important with moisture-sensitive materials. Vijay Chaudhry, Chief Executive Officer, Bry-Air (Asia) Pvt. Ltd., highlights the role of controlled drying and low-dew-point air in achieving consistent material conditions before extrusion, particularly for polymers such as PBT and PA/nylon. For FRLS and ZHFR compounds, he also points to dehumidification as part of material conditioning before processing.
XLPE presents another set of requirements. Dispersion, temperature control and cooling influence the final properties of the material, while thermoset applications bring curing into the machinery equation. Rubber, silicone and other specialised materials similarly require process-specific approaches.
For machinery builders, this makes the extrusion line an engineered process system rather than a generic platform. Screw geometry, feeding characteristics, melt temperature, pressure, tooling and cooling have to work together within the processing window of the material.
Curing technology adds another dimension to the machinery equation. Thermoset, rubber and silicone applications can require different curing approaches, including steam, infrared and continuous vulcanisation systems. The machinery challenge therefore extends beyond melt preparation and shaping to the controlled development of the cable’s final material properties. Reji Koshy Daniel, Executive Director, Royle Extrusion Systems Private Limited, adds: “Cable manufacturers may be wise to discuss their requirements with extrusion system manufacturers who offer all types of curing system solutions.”
This also makes process engineering increasingly important alongside mechanical design. A machine can have sufficient installed capacity, but its commercial performance depends on how consistently it maintains the required process conditions.
Flexibility Has Limits Manufacturers increasingly want extrusion lines that can accommodate changing products and materials. This is partly an economic requirement. A line that can process several product families can spread capital investment across a broader production base and reduce the risk of equipment becoming underutilised as product demand changes.
Vivek Mehta, Managing Director, Sai Extrumech Pvt. Ltd., points to plants increasingly moving between materials such as PVC, HFFR and XLPE. Vivek Kohli, Director, Supermac Industries (India) Limited, says the company designs lines with configurable single-, dual- and triple-extrusion arrangements, depending on the product and customer requirement.
Flexibility, however, has limits. A line designed to accommodate multiple materials still needs appropriate screws, tooling, temperature settings and downstream configurations. More demanding applications can therefore require dedicated arrangements rather than simply broader machine capability.
Sandip Bhuva, CEO, Rajoo Bausano Extrusion Private Limited, describes movement toward modular and configurable systems. He relates equipment configuration to material, product geometry and production requirements rather than assuming a standard line for every application. Rajoo Bausano’s contribution focuses substantially on compounding extrusion.
Flexibility does not mean that every material can be processed under the same conditions. It means that the machinery can accommodate different defined process windows without compromising stability.
The balance is between platform flexibility and application-specific optimisation. The more specialised the cable, the greater the importance of getting that balance right.
Speed Is Useful Only When the Process Remains Stable Line speed remains a major performance parameter. The more important distinction is between nominal speed and productive output.
As throughput increases, the available process window can become narrower. Small changes in feeding, melt temperature, pressure or cooling can affect dimensional stability and product quality. The resulting scrap, adjustment time or downtime can offset the additional output obtained from running faster.
Dr. Lahti puts the trade-off directly: “The most common trade-off arises when manufacturers seek higher line speeds without compromising dimensional accuracy, concentricity or insulation quality.” Maillefer’s position is that output stability is a major contributor to production economics. Stable extrusion across the operating range can support higher productivity with lower scrap, fewer operator interventions and stronger overall equipment effectiveness.
Sandip Bhuva makes a similar point from the compounding extrusion side. As throughput increases, the process window narrows, and vari
Source: wirecable